
Condensate Pump: Operating Principle, Types and Energy Savings
Learn how condensate pumps return condensate to the boiler house to save fuel and water, and how electric and mechanical pumps differ.
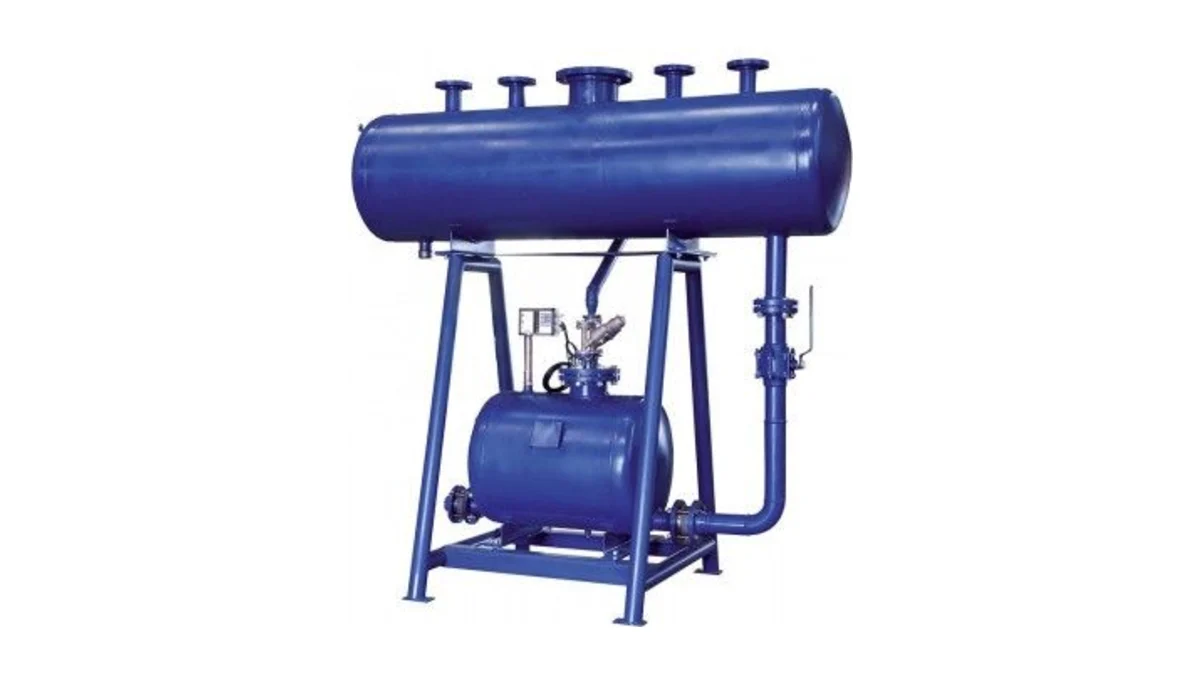
Condensate formed in steam systems is still hot, treated water; sending it to drain wastes both energy and water. A condensate pump collects condensate from steam-using equipment and pumps it back to the boiler house or another point of use. It makes condensate return possible where condensate cannot flow back by gravity.
This article covers why condensate pumps matter, how they work, the differences between electric and mechanical types, and where they are used.
Why Is Condensate Return Important?
- Energy savings: Hot condensate raises the boiler feedwater temperature, so the boiler burns less fuel to produce the same steam.
- Water and chemical savings: Condensate is water that has already been treated and conditioned. Recovering it reduces make-up water, water treatment and chemical consumption.
- Process efficiency: Removing condensate from equipment regularly prevents heating surfaces from waterlogging and maintains heat transfer.
How Does a Condensate Pump Work?
- Condensate from steam-using equipment flows by gravity into the pump receiver or body.
- When the condensate reaches a set level, the pump starts automatically.
- The pump delivers condensate to the boiler feed tank or another point of use; when the level drops it stops and a new filling cycle begins.
Electric vs Mechanical Condensate Pumps
| Feature | Electric condensate pump | Mechanical condensate pump |
|---|---|---|
| Drive | Electric motor-driven (usually centrifugal) pump | Steam or compressed air/gas pressure |
| Construction | Receiver tank, level control and pump | Pressure body with float mechanism and inlet/outlet check valves |
| Hot condensate | Risk of cavitation with condensate near saturation | No impeller, so no cavitation problem |
| Power supply | Electrical connection required | No electricity required |
How a mechanical condensate pump works
As condensate fills the body, the float rises. At a set level the mechanism closes the exhaust valve and opens the motive valve; steam or compressed air entering the body pushes the condensate out through the outlet check valve. When the body is empty the float falls, the motive valve closes, the exhaust valve opens and the body starts filling again.
Why does cavitation matter?
Condensate close to saturation temperature flashes easily as pressure drops at the suction of a centrifugal pump. The vapour bubbles collapse on the impeller, causing noise, vibration and impeller erosion. With electric pumps, the available suction head and the pump’s suitability for the condensate temperature must therefore be checked. Mechanical pumps are not affected by this problem.
Applications
- Power plants and refineries
- Chemical plants
- Food processing plants
- Textile and paper mills
- Any steam installation where condensate cannot return to the boiler house by gravity
Frequently Asked Questions
When is a condensate pump needed?
When condensate cannot return to the boiler house by gravity or by steam trap discharge pressure, for example when the boiler house is higher or far away, or when there is back pressure in the return line.
What is the advantage of a mechanical condensate pump?
It needs no electricity, has no impeller and therefore no cavitation problem with hot condensate, and is driven by steam or compressed air.
What does condensate recovery deliver?
Hotter feedwater means lower fuel consumption, and reusing treated water reduces make-up water and treatment chemical consumption.
Conclusion
Condensate pumps recover the heat and treated water in condensate, saving fuel and water in steam systems. Choose an electric or mechanical type according to the condensate temperature, flow and delivery head of the application. See pump options in our pumps and systems product group, or ask the ORFA technical team about your condensate return system.
Buy pumps online
Browse products on or-fa.com, our export store, see prices in USD and order online.
Buy Online →Request a QuoteAsk on WhatsAppRelated product group
Pumps and Systems →Technical support
Talk to our team to choose the right product.
+90 224 444 67 32[email protected]
Related Articles
Let’s choose the right product for your project
Buy from our online store or request a project-specific quotation.